In optical thin-film deposition, vacuum coating, and semiconductor functional film manufacturing, equipment procurement and process teams consistently prioritize core performance metrics for vacuum glove boxes. Key factors such as oxygen and moisture control accuracy, system leak rate, stainless steel material grade, and ESD safety performance are widely regarded as the primary selection criteria. These critical specs ensure stable coating quality, cleanroom compliance, and qualified product yield, forming the basic guarantee for standardized production.
However, most manufacturers overlook two pivotal efficiency parameters that directly restrict continuous production capacity: antechamber size and vacuum pumping speed. In practical industrial scenarios, many production lines face a common dilemma: all glove box quality indicators meet industrial standards, yet the overall production throughput and equipment utilization rate remain low. The root cause is not insufficient coating host performance, but unreasonable antechamber configuration that creates persistent material transfer bottlenecks, limiting the full productivity of vacuum coating systems.
For automated continuous vacuum coating lines, the vacuum glove box antechamber acts as the core transfer hub for substrate and jig circulation. Its volumetric design and evacuation efficiency directly determine single-batch transfer cycle time, hourly production output, and long-term manufacturing costs. This professional guide explores the industrial selection logic of antechamber size and pumping speed, providing actionable optimization strategies for process engineers and procurement decision-makers to maximize production tact time and line efficiency.
Widespread Industrial Selection Pitfall: Prioritizing Quality Specs Over Production Throughput
A prevalent mistake in glove box procurement is over-reliance on static main-chamber performance while ignoring dynamic throughput capabilities. Most buyers focus heavily on steady-state O₂/H₂O control below 0.1 ppm, ultra-low system leakage, corrosion-resistant stainless steel construction, and cleanroom compatibility. These parameters define the quality bottom line of thin-film coating processes and effectively avoid defective products caused by atmosphere contamination.
Nevertheless, standard laboratory-grade glove boxes with conventional antechamber designs are only suitable for intermittent sampling and small-batch R&D. Equipped with compact transfer chambers and basic pumping systems, they cannot adapt to the high-frequency material transfer demands of 24/7 continuous industrial production. Frequent loading and unloading requires repeated vacuum evacuation and inert gas purging, generating massive non-value-added downtime. Even with high-precision coating equipment, mismatched glove box antechamber configurations will inevitably lead to idle equipment and suppressed production output.
Different from laboratory discontinuous operation, industrial vacuum coating production pursues uninterrupted material circulation and stable tact time balance. The main chamber maintains a ultra-clean process atmosphere to guarantee coating yield, while the antechamber undertakes all external material exchange work. Once the transfer efficiency fails to match the production rhythm, the entire coating line will face the problem of “high-end equipment, low-end productivity”.
How Antechamber Size Determines Continuous Mass Production Capacity
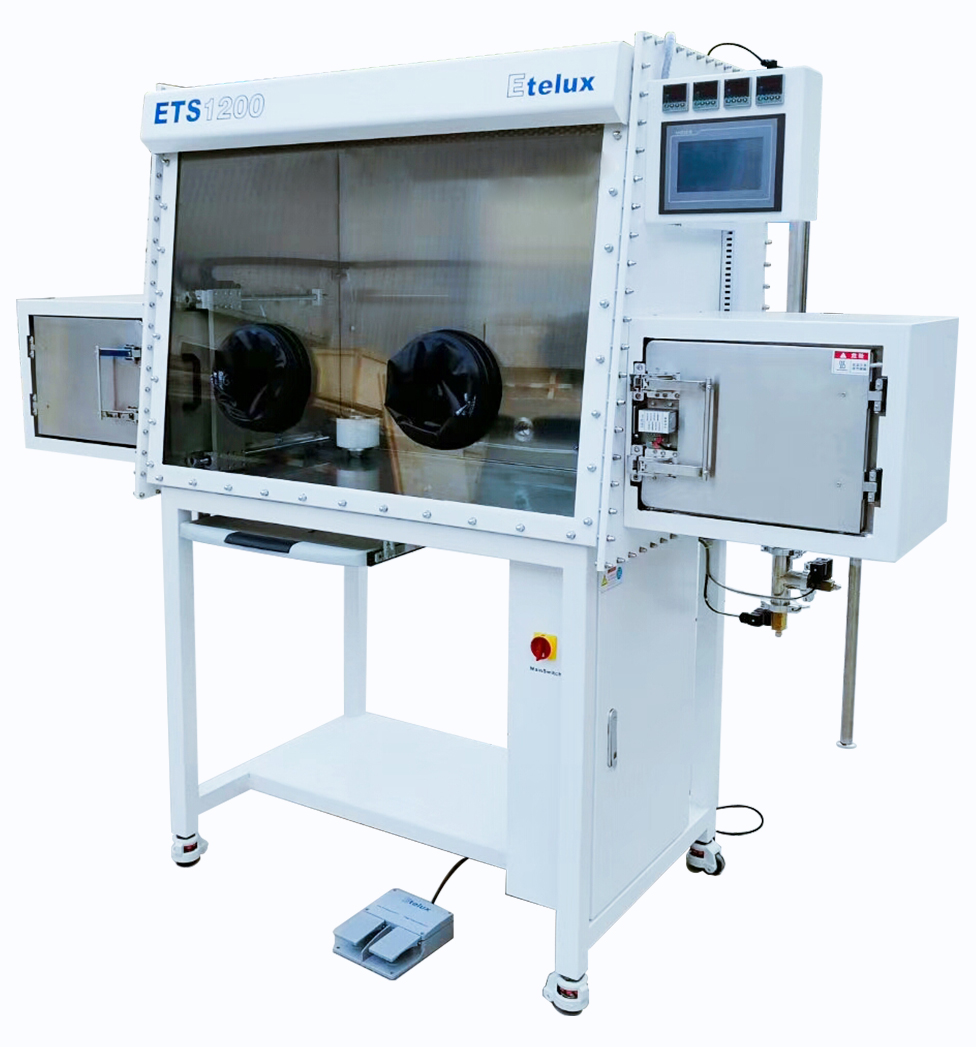
The vacuum glove box antechamber (transfer chamber) is designed to isolate ambient air, moisture, and particulate contaminants while enabling safe and efficient internal and external transmission of substrates, production jigs, and turnover trays. Many manufacturers choose compact standard antechambers to cut upfront equipment costs, which turns into a long-term production capacity loss in mass manufacturing scenarios.
Antechamber volumetric size affects vacuum coating production efficiency from two core dimensions:
1. Batch Loading Capacity Reduces Repetitive Transfer Downtime
Small-volume standard antechambers can only accommodate a small number of substrates or single groups of jigs, requiring dozens of repeated evacuation and purging cycles per production shift. Each material transfer involves complete atmospheric replacement, resulting in accumulated cycle delays and severely reduced hourly throughput. Industrial customized large-capacity antechambers support full-tray and full-batch one-time loading, drastically cutting transfer frequency, compressing single-batch production cycles, and significantly improving continuous production efficiency.
2. Optimized Chamber Volume Stabilizes Process Atmosphere Consistency
Antechamber configuration follows the balance principle of “matching volume and pumping capacity” — oversized or undersized chambers both hinder production stability. An oversized antechamber paired with low-power pumping units leads to prolonged evacuation time and incomplete gas replacement; an undersized chamber cannot meet large-batch production demands and triggers frequent atmosphere switching.
Professionally customized industrial antechambers are tailored according to actual substrate dimensions, jig structures, and production batch specifications. While maximizing single-batch loading capacity, it minimizes main chamber atmosphere fluctuations caused by frequent transfers. Stable internal O₂/H₂O levels and airflow environments effectively avoid thin-film color deviation, poor adhesion, and batch inconsistency defects caused by repeated material exchange.
Vacuum Pumping Speed: The Core Dynamic Parameter Controlling Production Tact Time
If antechamber size is the hardware foundation of production throughput, operational vacuum pumping speed is the core dynamic factor that determines real production tact time. Pumping speed refers to the actual time required to evacuate the antechamber from atmospheric pressure to the target process vacuum, which directly defines the shortest interval of each material transfer cycle. It is also the most easily overlooked key parameter in industrial glove box procurement.
A typical procurement trap in the vacuum equipment industry is focusing only on the equipment’s ultimate vacuum degree rather than the practical pumping speed under real production load. Multiple glove box models with the same ultimate vacuum spec often present huge differences in actual production efficiency due to mismatched pumping power and chamber volume.
1. Working Pumping Speed Directly Defines Batch Cycle Efficiency
The continuous vacuum coating workflow forms a closed-loop production cycle: finished product unloading → antechamber vacuum evacuation → inert gas purging and replacement → new substrate loading → vacuum coating processing → next batch circulation. The running time of the coating process itself is fixed and unadjustable, making antechamber pumping and purging latency the only optimizable bottleneck in the entire production link. Higher and more stable pumping speed shortens material turnover intervals, increases effective production batches per hour, and realizes continuous line capacity improvement without upgrading core coating equipment.
2. Stable Evacuation Performance Ensures Batch Coating Consistency
Industrial-grade vacuum glove boxes adopt high-precision pressure sensing modules and balanced pumping systems, achieving uniform, repeatable evacuation and gas replacement. In contrast, ordinary standard glove boxes have unstable pumping rates, prone to incomplete vacuum evacuation and residual air contamination. Insufficient purging leaves trace oxygen and moisture in the antechamber, which enters the main chamber with material transfer, causing thin-film pinholes, uneven coating thickness, and inconsistent product quality between batches.
3. Volume-Power Matching Reduces Long-Term Operational Costs
Mismatched antechamber and pumping unit configurations bring unnecessary operational losses and maintenance risks. A high-power pumping system matched with a small chamber causes energy redundancy and accelerated mechanical wear; a low-power pump paired with a large-volume antechamber leads to prolonged evacuation, unqualified vacuum degree, and incomplete gas purification. Industrial production-grade glove boxes adopt precise volume-power matching design, which balances rapid transfer efficiency, stable operation, low energy consumption, and long service life, perfectly adapting to 24/7 continuous mass production.
Industrial-Grade Antechamber Selection Standards for Vacuum Coating Lines
Combined with the actual production characteristics of optical coating, semiconductor thin-film deposition, and functional film manufacturing, we summarize practical and actionable selection specifications for engineers and procurement decision-makers to balance process quality, production efficiency, and comprehensive cost:
1. Adopt customized antechamber sizing instead of generic standard chambers: Configure antechamber volume based on actual substrate sizes, full-tray loading specifications, and hourly production targets to realize one-time full-batch transfer, eliminate repetitive operation latency, and adapt to continuous production rhythm.
2. Prioritize load-based working pumping speed over static ultimate vacuum: Take the actual evacuation time from atmospheric pressure to process vacuum under production load as the core evaluation standard, rather than only referring to static laboratory ultimate vacuum data.
3. Equip dual-stage pumping and multi-cycle inert gas purging systems: Industrial production models support two-stage vacuum evacuation and 2–3 times circulating gas replacement, thoroughly removing residual air and moisture while ensuring efficient transfer, meeting ultra-low O₂/H₂O process requirements.
4. Implement volume and pumping power balanced design: Avoid mismatched configurations that restrict productivity, and realize three-dimensional optimization of production throughput, process stability, and long-term operational cost for continuous vacuum coating production.
Conclusion: Efficient Antechamber Configuration Maximizes Manufacturing Profitability
In the homogenized vacuum glove box market, basic parameters such as material grade, leak rate, and gas purification accuracy have become industry standard configurations and can no longer form production advantages. The differentiated antechamber design and matched pumping speed are the key factors that distinguish laboratory equipment from industrial mass production equipment.
For vacuum coating enterprises, equipment procurement should not only focus on process qualification compliance but also take long-term production tact time optimization and line utilization improvement as core goals. A standard-compliant but low-efficiency glove box will form an invisible production bottleneck, resulting in long-term output loss, labor waste, and delayed order delivery — with comprehensive losses far exceeding the initial equipment price difference.
The industrial value of professional vacuum glove boxes lies not only in building a stable ultra-clean process environment but in matching efficient material transfer capabilities with continuous production needs. Optimized antechamber and pumping system configurations can fully release the performance of vacuum coating host equipment, effectively reduce production costs, and create sustainable productivity benefits for thin-film manufacturing lines.